Die Spring Selection Guide: OD, ID, Free Length, Load Class, End Type
A die spring is defined by five parameters and one interface: outer diameter (OD), inner diameter (ID), free length, load class, and end type — plus winding direction, which determines how the spring seats in its pocket. A spring can carry the correct load rating and still be the wrong part if any of the remaining numbers is left unverified.
This guide walks through those parameters in the order a tooling engineer or maintenance buyer should verify them, using the dimensional ranges and load-class conventions that govern ISO 10243, JIS B5012, and American Standard (Inch series) die springs. It also explains why the same parameter list decides whether a mould component programme can run for years on one supply source, instead of being re-qualified at every reorder.
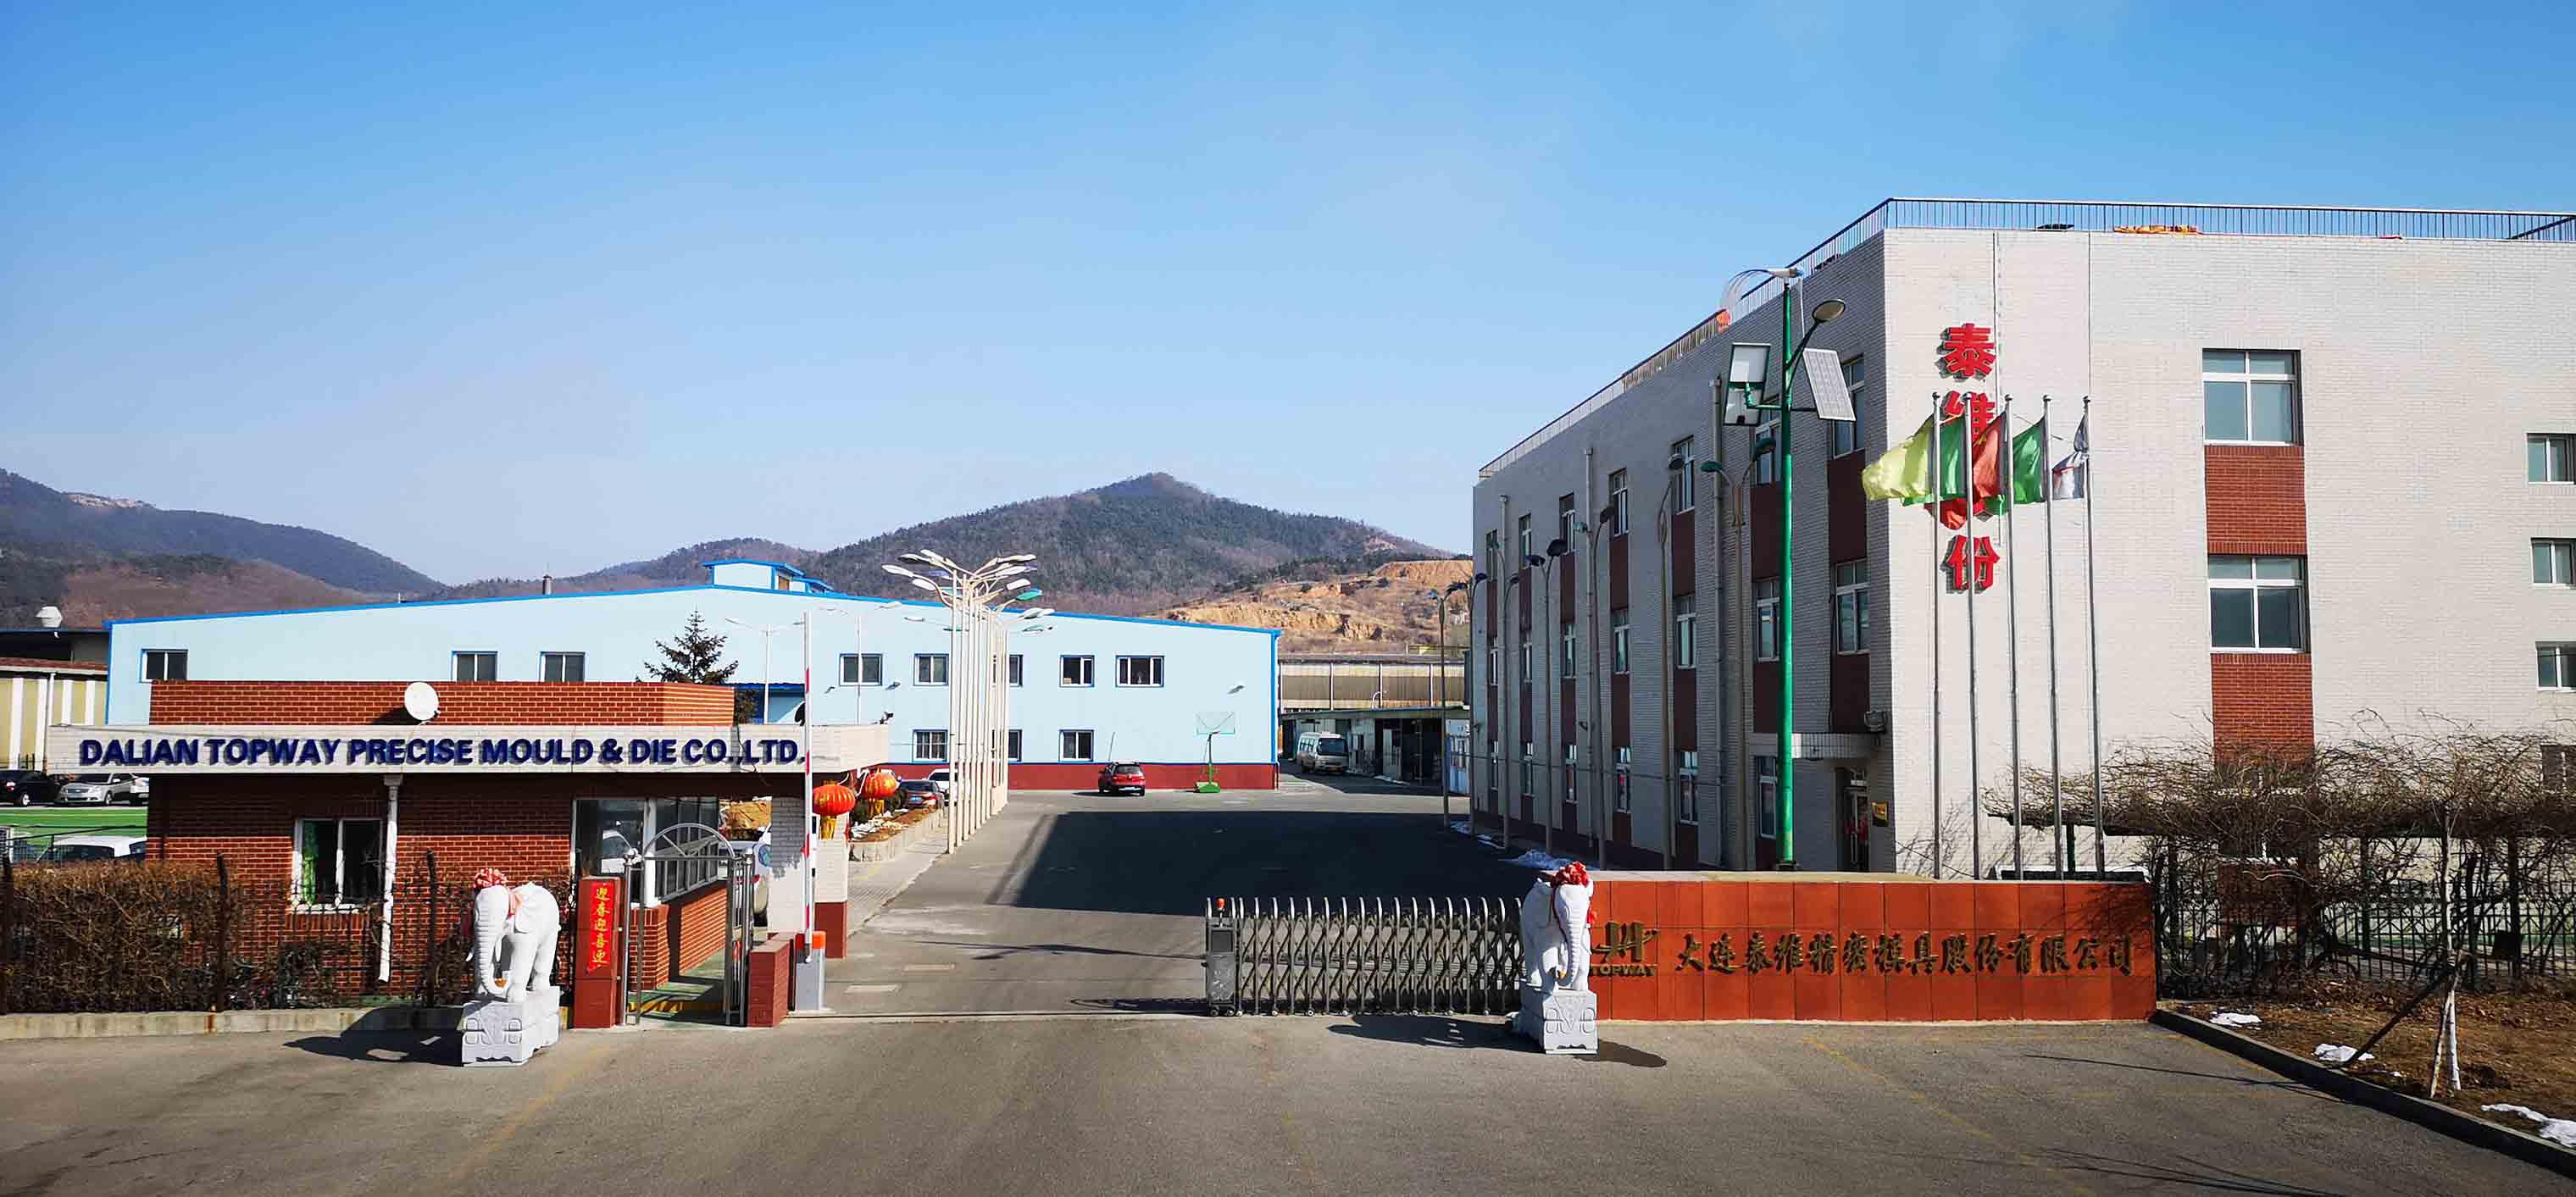
TOPWAY SPRINGS is the spring brand of Dalian TopWay Precise Mould & Die Co., Ltd., a Chinese precision mould and die component manufacturer founded in 2012. The company operates a 16,500 m² facility in Dalian with an annual production capacity of 3,600,000 pieces, exports approximately 50% of its output to the EU and USA, and manufactures die springs from 55CrSi chrome silicon steel across ISO 10243, JIS B5012, and American Standard (Inch series) specifications.
Why the Same Nominal Size Is Not the Same Spring
Most die spring problems that reach a buyer are not caused by a wrong load rating. They are caused by a parameter that was assumed rather than measured. Three patterns account for the majority of repeat issues, and all three can be closed before the purchase order is issued.
1. Diameter fit: OD into the bore, ID over the rod
A die spring has two interfaces, not one. The outer diameter must clear the pocket bore, and the inner diameter must clear the guide rod, pin, or boss that runs through the spring. Buying on OD alone leaves the ID unverified, and an undersized bore clearance produces the classic symptoms of a spring that is compressed but also squeezed — marked coils, localised wear, and a service life far below the published figure.
2. Free length is not installed length
A spring with a 50 mm free length does not operate at 50 mm. It is installed at a preloaded height, then compressed through the working stroke of the tool. Selecting free length from pocket depth alone produces a spring that runs at excessive deflection, and excessive deflection is the fastest route to permanent set and fatigue fracture. It also invalidates the published life figures, because those figures are quoted inside a defined deflection band.
3. Load class read from colour alone
Colour coding is fast and practical — until two standards coexist in the same plant or the same supply chain. ISO 10243 and JIS B5012 assign different colours to comparable load levels, and the American Standard (Inch series) uses a third colour set. A spring identified only by colour is a specification waiting to be mis-ordered.
Standards note. ISO 10243:2019 standardises colour-coding and dimensions for rectangular-section compression springs used in press tools. JIS B5012 specifies allowable tolerances of the inner and outer diameters of springs, and its focus differs from ISO 10243, which centres on mounting hole dimensions. Because the two systems do not assign the same colour to the same load level, colour alone is not a safe identification method in mixed-standard tooling.
The consequence for long-term supply is cumulative. Every unverified parameter is discovered at the press rather than at the drawing stage, and each discovery triggers a re-qualification cycle, an unplanned order, and a window of downtime that a documented, stocked supply programme would have absorbed without a stoppage.
Industry Background: Why Long-Term Supply Now Outweighs First-Order Price
The global industrial springs market is projected to reach USD 7.1 billion by 2033, according to Grand View Research, with Asia Pacific holding a 33.4% revenue share in 2024. Demand is anchored in end markets that consume springs continuously rather than occasionally: the automotive stamping market alone was valued at USD 87.98 billion in 2024, and automotive stamping dies, plastic injection moulds and die casting tooling are among the heaviest users of rectangular-section compression springs.
Trade data shows the same picture from a different angle. The US import HS code for helical springs of iron or steel is 732020 — a single code that covers both round-wire and rectangular-section products. Customs records therefore cannot separate a precision die spring from a suspension spring, which means the technical identity of a die spring shipment depends on supplier documentation rather than on a trade code.
For buyers, two pressures now run in parallel. Cost pressure pushes sourcing toward factory-direct manufacturing, most of which is concentrated in Asia. Continuity pressure pushes the other way: a stamping die or injection mould that runs for years needs the same OD, ID, free length and load class available on every reorder, with the same material grade and end treatment. A cheaper spring that cannot be re-ordered in an identical specification is not a saving; it is a re-engineering project.
This is where the parameters in this guide become commercial rather than purely technical. A supplier that documents and holds them is a long-term mould component supplier. A supplier that quotes only a size is a transactional vendor, and the difference shows up on the second or third order — not the first.
The Five Parameters, and How to Verify Each One
Parameter 1 — Outer diameter and inner diameter
Diameter ranges differ by standard, and the differences matter when a tool originally designed around one system is replenished from another. The table below summarises the coverage of the three main die spring systems.
| Standard | Outer diameter (OD) | Inner diameter (ID) | Free length |
|---|---|---|---|
| ISO 10243 (CIF / CIL / CIM / CIH / CIB series) | 10 mm to 63 mm | 5 mm to 38 mm | 25 mm to 305 mm |
| JIS B5012 (CSWF / CSWL / CSWM / CSWH / CSWB / CSWG series) | 6 mm to 70 mm | 3 mm to 38.5 mm | 10 mm to 350 mm |
| American Standard (Inch series) | 10 mm to 51 mm | 4.76 mm to 25.4 mm | 25 mm to 305 mm |
Verification points for diameters:
- Measure the pocket bore and the guide rod or pin, and use the existing spring only as a cross-check rather than as the specification.
- Confirm both OD and ID on the finished part, including the powder coating, since the coating is part of the delivered dimension.
- Record the part number convention used by the selected series — for example CSWF10-30 in the JIS B5012 range or CIF20-25 in the ISO 10243 range — so a reorder cannot drift into a different load tier.
- Check that the required OD and ID combination is inside the standard range, or flag it as a custom item before quoting.
Parameter 2 — Free length, preload and working deflection
Free length is the starting point of a calculation, not the installed dimension. The working sequence is: free length minus preload equals installed length; installed length minus working stroke equals the compressed length at full press travel.
- Preload. An initial preload of 5% to 10% of free length is the standard recommendation. It removes internal play and prevents the shock loading, chatter and lateral buckling that occur when a spring is allowed to run loose inside its pocket.
- Working deflection. TOPWAY die springs deliver a fatigue life of 3 to 5 million compression cycles when operated within a 12% to 40% compression stroke. For long-life applications, the recommended working band sits at the conservative end of that range, around 30% to 35% of free length.
- Solid height check. Free length must leave enough installed height that the spring never reaches solid before the press reaches bottom dead centre.
Common verification gap: deflection. Many buyers verify OD, ID and free length at goods-in, then discover during commissioning that the working stroke exceeds the recommended percentage of free length. Deflection is a specification value, not a press setting, and it belongs on the purchase specification next to the dimensions.
Parameter 3 — Load class and colour code
Load class defines how much force a spring produces at a given deflection. Each standard expresses it through a series of tiers and a colour system, and the colours are not transferable between standards.
| Standard | Load tiers and colour codes |
|---|---|
| ISO 10243 | CIF super minimal load (light green), CIL light duty load (green), CIM medium duty load (blue), CIH heavy duty load (red), CIB extra heavy duty load (yellow) |
| JIS B5012 | CSWF minimal load (yellow), CSWL light load (blue), CSWM medium load (red), CSWH heavy load (green), CSWB extra heavy load (brown), CSWG super heavy load (black) |
| American Standard (Inch series) | Medium duty (blue), medium heavy duty (red), heavy duty (gold), extra heavy duty (green) |
The trap is visible in the table itself: blue identifies a medium duty spring in the ISO 10243 series but a light load spring in the JIS B5012 series, and green moves from light duty in ISO to heavy load in JIS. Where a plant runs both systems, load class should be confirmed by part number, colour code and load-deflection data together — never by colour alone. Powder coating is applied as a high-adhesion coating, so the colour also resists stamping coolants and abrasion without chipping into precision die cavities.
Parameter 4 — End type
Two end configurations are available across the range: closed and ground, and closed un-ground. Both are closed-coil ends; the difference is whether the end face is ground flat and square to the spring axis.
- Closed and ground ends. Grinding produces squareness and a perpendicular load distribution, which keeps the spring centred in the pocket and reduces lateral deflection wear that shortens tool life. This is the correct choice for high-cycle and high-load positions.
- Closed un-ground ends. A lower-cost configuration suited to moderate loads, limited deflection, and pockets that already provide adequate guiding.
Parameter 5 — Winding direction, material and surface treatment
Three attributes are frequently left off a purchase specification because they do not appear on a simple dimensional drawing: winding direction, material grade, and surface treatment.
- Winding direction. Right-hand or left-hand winding is available. Direction should be carried over from the original drawing, because it affects how the spring behaves against a rotating or indexing load path.
- Material grade. The range is manufactured in 55CrSi (chrome silicon) oil-tempered alloy steel. Compared with standard carbon spring steels, 55CrSi offers higher tensile strength, a superior fatigue limit, and stronger resistance to permanent set and thermal relaxation under cyclic heavy loading.
- Cross-section geometry. A rectangular, trapezoidal wire section stores 30% to 50% more energy than a round-wire spring of the same footprint, which is why rectangular wire dominates press tool and mould applications where pocket space is fixed.
- Shot peening and multi-stage tempering. Controlled shot peening introduces compressive residual stress at the wire surface to resist micro-crack propagation, and multi-stage tempering stabilises the structure against thermal relaxation. Together, these processes support the 3 to 5 million cycle fatigue figure under high-frequency stamping conditions.
- Powder coating. The finish is a durable powder coating used both for corrosion and abrasion resistance and for colour identification of load class. It is a functional surface, not a decorative one.
For traceability, mill test certificates and material heat-number traceability are provided for raw materials, and the finished product complies with ISO 10243, JIS B5012, and American Standard (Inch series). Total coils and active coils are specified according to the spring design, which means the coil count is a design output of the selected dimensions and load class rather than an independent choice.
A Seven-Step Verification Sequence
The sequence below can be used as a pre-order checklist. Each step closes one parameter before the next is fixed, which keeps the specification from drifting between quotation and delivery.
- Measure the pocket and the rod. Record pocket bore, pocket depth, guide rod or pin diameter, and available spring travel. Do not size from a used spring alone.
- Establish the required force and deflection. Convert the tool requirement into force at working deflection, then read the load class that meets it with margin for preload.
- Fix the free length. Free length equals installed length plus preload plus working stroke, checked against pocket depth so the spring never reaches solid height.
- Confirm the standard and the part number. Decide whether the tool follows ISO 10243, JIS B5012, or the American Standard, then select the part number from that series so the load class is unambiguous.
- Choose the end type. Closed and ground for high-cycle, high-load and tight-squareness positions; closed un-ground where the duty allows it.
- Lock the remaining attributes. Winding direction, material grade (55CrSi), powder coating colour, deflection limit, and the documentation package covering mill test certificates and heat-number traceability.
- Qualify, then standardise. Validate the first batch, then convert the approved specification into a standing item so repeat orders carry no specification risk and no re-qualification cost.
Where the Parameter Set Changes by Application
The five parameters are universal, but the weight given to each one shifts with the tool and the duty cycle.
Automotive stamping dies. High stroke rates and long production runs put fatigue life first. The specification typically moves toward heavier load classes, closed and ground ends, and a long-life deflection target of roughly 30% to 35% of free length, with preload applied during installation.
Plastic injection moulds. Springs in injection moulds are judged by resistance to thermal relaxation as much as by cycle count. Medium duty classes, consistent preload, and material grade become the decisive parameters, while free length is set by the ejector plate travel.
Die casting tooling. Heat exposure combined with short, forceful strokes pushes selection toward extra heavy duty classes and ground end faces, where perpendicular load distribution protects the pocket from uneven wear.
MRO replacement in large die sets. Here the requirement is drop-in interchangeability. OD, ID, free length and load class must match the installed population, which is why standards compliance and batch documentation carry more weight than a nominal size match — a replacement spring that changes the load class changes the behaviour of the whole tool.
Industrial automation, elevators, valves and heavy-duty energy systems. Rectangular die springs are also specified outside press tools. The same parameters apply, but the duty cycle is often lower and the deciding variables are usually winding direction, end type and coating durability.
Comparison: What Differs Between the Three Standards
The comparison below is written from a buyer perspective. It shows what each standard governs, how far its coverage extends, and what that means when the same specification has to be re-supplied over several years.
| Standard | Primary dimensional focus | Coverage in the TOPWAY range | Colour coding | What it means for long-term supply |
|---|---|---|---|---|
| ISO 10243 | Mounting hole dimensions and colour coding for rectangular-section press tool springs | OD 10–63 mm; ID 5–38 mm; free length 25–305 mm | Five load tiers, super minimal to extra heavy duty | An international reference for press tool springs; a specification written in ISO terms transfers cleanly between tools built to the same standard. |
| JIS B5012 | Allowable tolerances of the inner and outer diameters of springs | OD 6–70 mm; ID 3–38.5 mm; free length 10–350 mm | Six load tiers, minimal to super heavy | The widest diameter and length coverage in the range; part-number confirmation is essential because the colour codes differ from ISO. |
| American Standard (Inch series) | Inch-based sizing for legacy and North American tooling | OD 10–51 mm; ID 4.76–25.4 mm; free length 25–305 mm | Four load tiers, medium duty to extra heavy duty | Useful for mixed fleets of imported and legacy dies; ID values in inch equivalents are the usual point of confusion during replacement. |
| Shared across all three | Material and finishing | 55CrSi chrome silicon steel; powder coating | Colour used for load identification | Consistency of material grade and finish across reorders is what keeps performance stable after the first qualification. |
A practical conclusion follows from the table: the standard chosen for a tool is less important than keeping the same standard, the same series code, and the same documentation in place across the life of the programme. Mixing standards introduces dimensional and colour ambiguity; mixing suppliers inside one standard introduces dimensional and metallurgical variation. Both increase the probability of an unplanned press stop.
Frequently Asked Questions
Do TOPWAY die springs comply with ISO 10243, JIS B5012 and American Standard, and can they replace installed springs without tool modification?
Yes. TOPWAY die springs comply with ISO 10243, JIS B5012, and American Standard (Inch series) specifications, and the range is manufactured to those dimensional, colour coding and load-deflection characteristics. Because installation dimensions and load classes follow the standard series, the springs function as direct replacements in existing tooling without modifying the mould or die design. Mill test certificates and material heat-number traceability are provided for the raw material, so the compliance claim is backed by documentation rather than by a catalogue description alone.
Can the factory manufacture custom rectangular die springs from drawings or physical samples?
Yes. TOPWAY customises springs according to client drawings or physical samples, and offers full OEM/ODM customisation covering wire profiles, load specifications, non-standard dimensions, colour-coded powder coatings, and private branding. Custom options sit alongside the standard ISO 10243, JIS B5012 and American Standard ranges rather than replacing them, so a programme can mix catalogue items for standard positions with engineered parts for non-standard pockets. Annual production capacity reaches 3,600,000 pieces.
What are the minimum order quantity, payment terms and delivery terms for die spring orders?
The minimum order quantity for die springs is 100 units. Quotations are issued and delivery is arranged under EXW-Factory terms for export orders. Payment is structured as 30% T/T in advance with the remaining 70% T/T due before shipment. Acceptance is performed by SGS as an independent third-party inspection body, which gives buyers a verifiable quality checkpoint before shipment rather than after arrival.
Can a physical sample be used to validate dimensions and load before committing to a long-term supply agreement?
Yes. Sample-based specification is one of the standard routes for non-standard or legacy parts: the sample is used to establish OD, ID, free length, wire profile, load rate and end type, and the resulting specification is then documented before serial production. This matters for long-term supply because it converts an undocumented replacement part into a repeatable part number. Combined with mill test certificates and heat-number traceability on the material, it gives a buyer a fixed reference point for every future reorder. Sending a drawing or a physical sample is the normal first step in that process.
What lead times apply to standard and custom die spring orders, and how does that support long-term mould component supply?
TOPWAY maintains a ready-to-ship inventory of standard ISO 10243, JIS B5012 and American Standard die springs, which supports dispatch within 24 to 48 hours for stock orders. Custom engineered or bulk OEM orders are produced on automated coiling lines with flexible scheduling, with typical delivery inside 2 to 3 weeks. For a long-term mould component programme, the combination of stocked standard items and a documented custom specification is what removes the two main sources of downtime risk: an unavailable standard size and an undocumented replacement. Buyers can request a quotation or a sample from the TOPWAY SPRINGS engineering and export team to start the qualification.
Conclusion
Die spring selection comes down to verifying five parameters in the correct order: outer diameter and inner diameter for the two fit interfaces, free length with preload and working deflection for the operating condition, load class for the force requirement, end type for squareness and load distribution, and winding direction, material grade and surface treatment for repeatability. Each parameter is defined differently depending on whether the spring is built to ISO 10243, JIS B5012, or the American Standard (Inch series), and the load-class colour codes between those systems are not interchangeable.
For buyers in the Decision and Execution stages, the value of that verification extends beyond a single order. A specification that records OD, ID, free length, load class, end type, material grade and deflection limit is a specification that can be re-supplied for years without re-qualification. That is the practical difference between sourcing a part and building a long-term mould component supply relationship.
Next Step: Verify Your Die Spring Specification
Send a drawing, a sample, or your current part number and operating deflection. The TOPWAY SPRINGS team will confirm the OD, ID, free length, load class, end type and standard series, then return a quotation and a sample plan.
Contact: Liya | Email: liya@chs-spring.com | Tel / WhatsApp: +86 151-4047-4905
Website: www.onetopway.com
Factory address: NO.49-1, GUSHAN STREET, ECONOMIC AND TECHNOLOGICAL DEVELOPMENT ZONE, DALIAN-116610, LIAONING, CHINA
Download the full product and capability catalogue: Dalian TopWay Catalogue (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.